Skip to content
getAdvantage

An agent for every area.A crew for your plant.

getAdvantage identifies anomalies in your operational data and prepares suitable actions. Your team decides what to approve.

  • Benjamin HellmichBenjamin HellmichCo-founder & CEO, AI and engineering
  • Marc LindnerMarc LindnerCo-founder, your contact for pilot plants
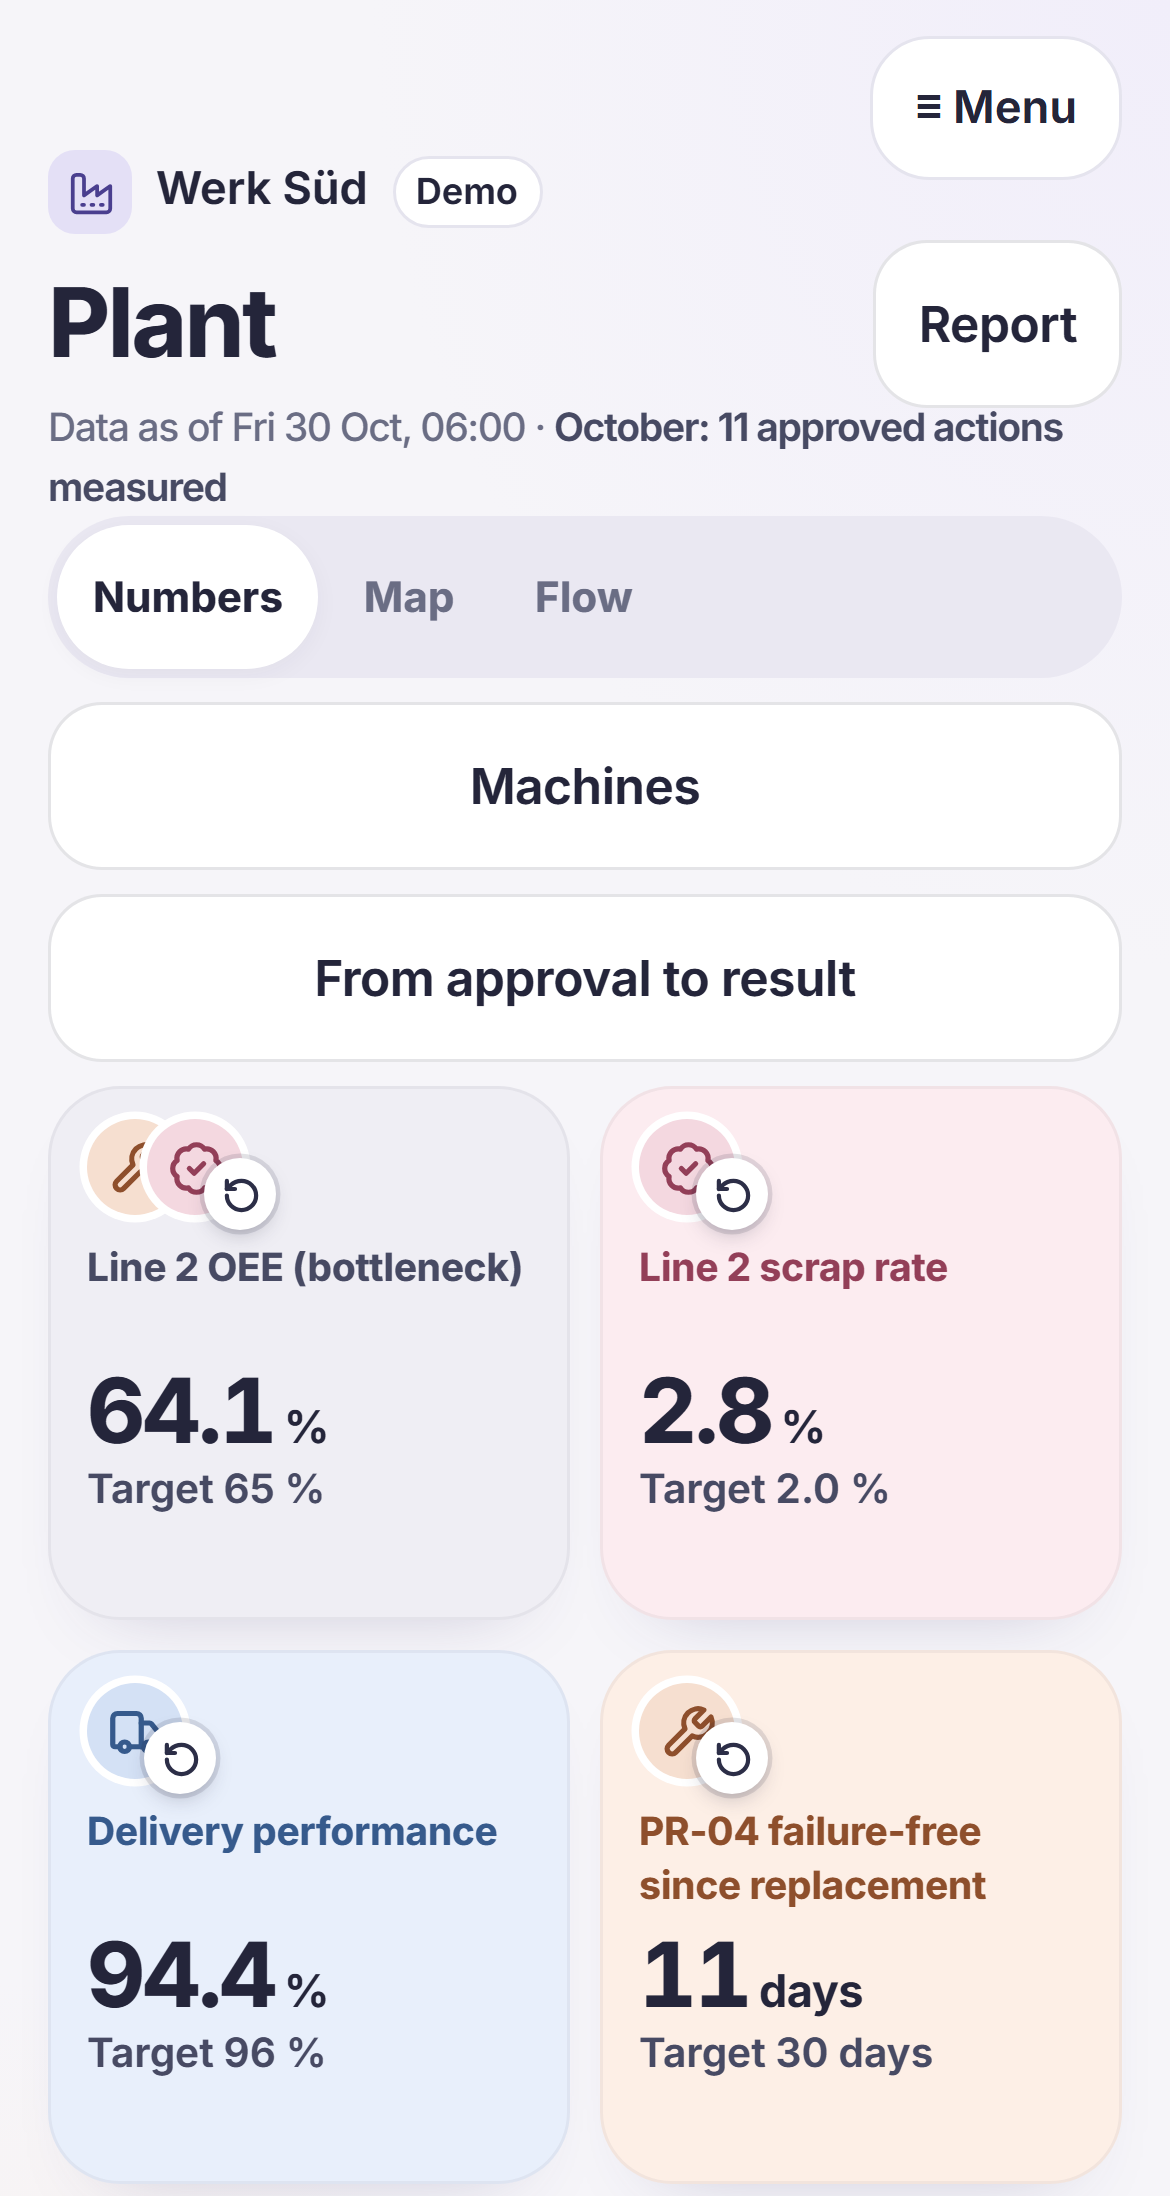
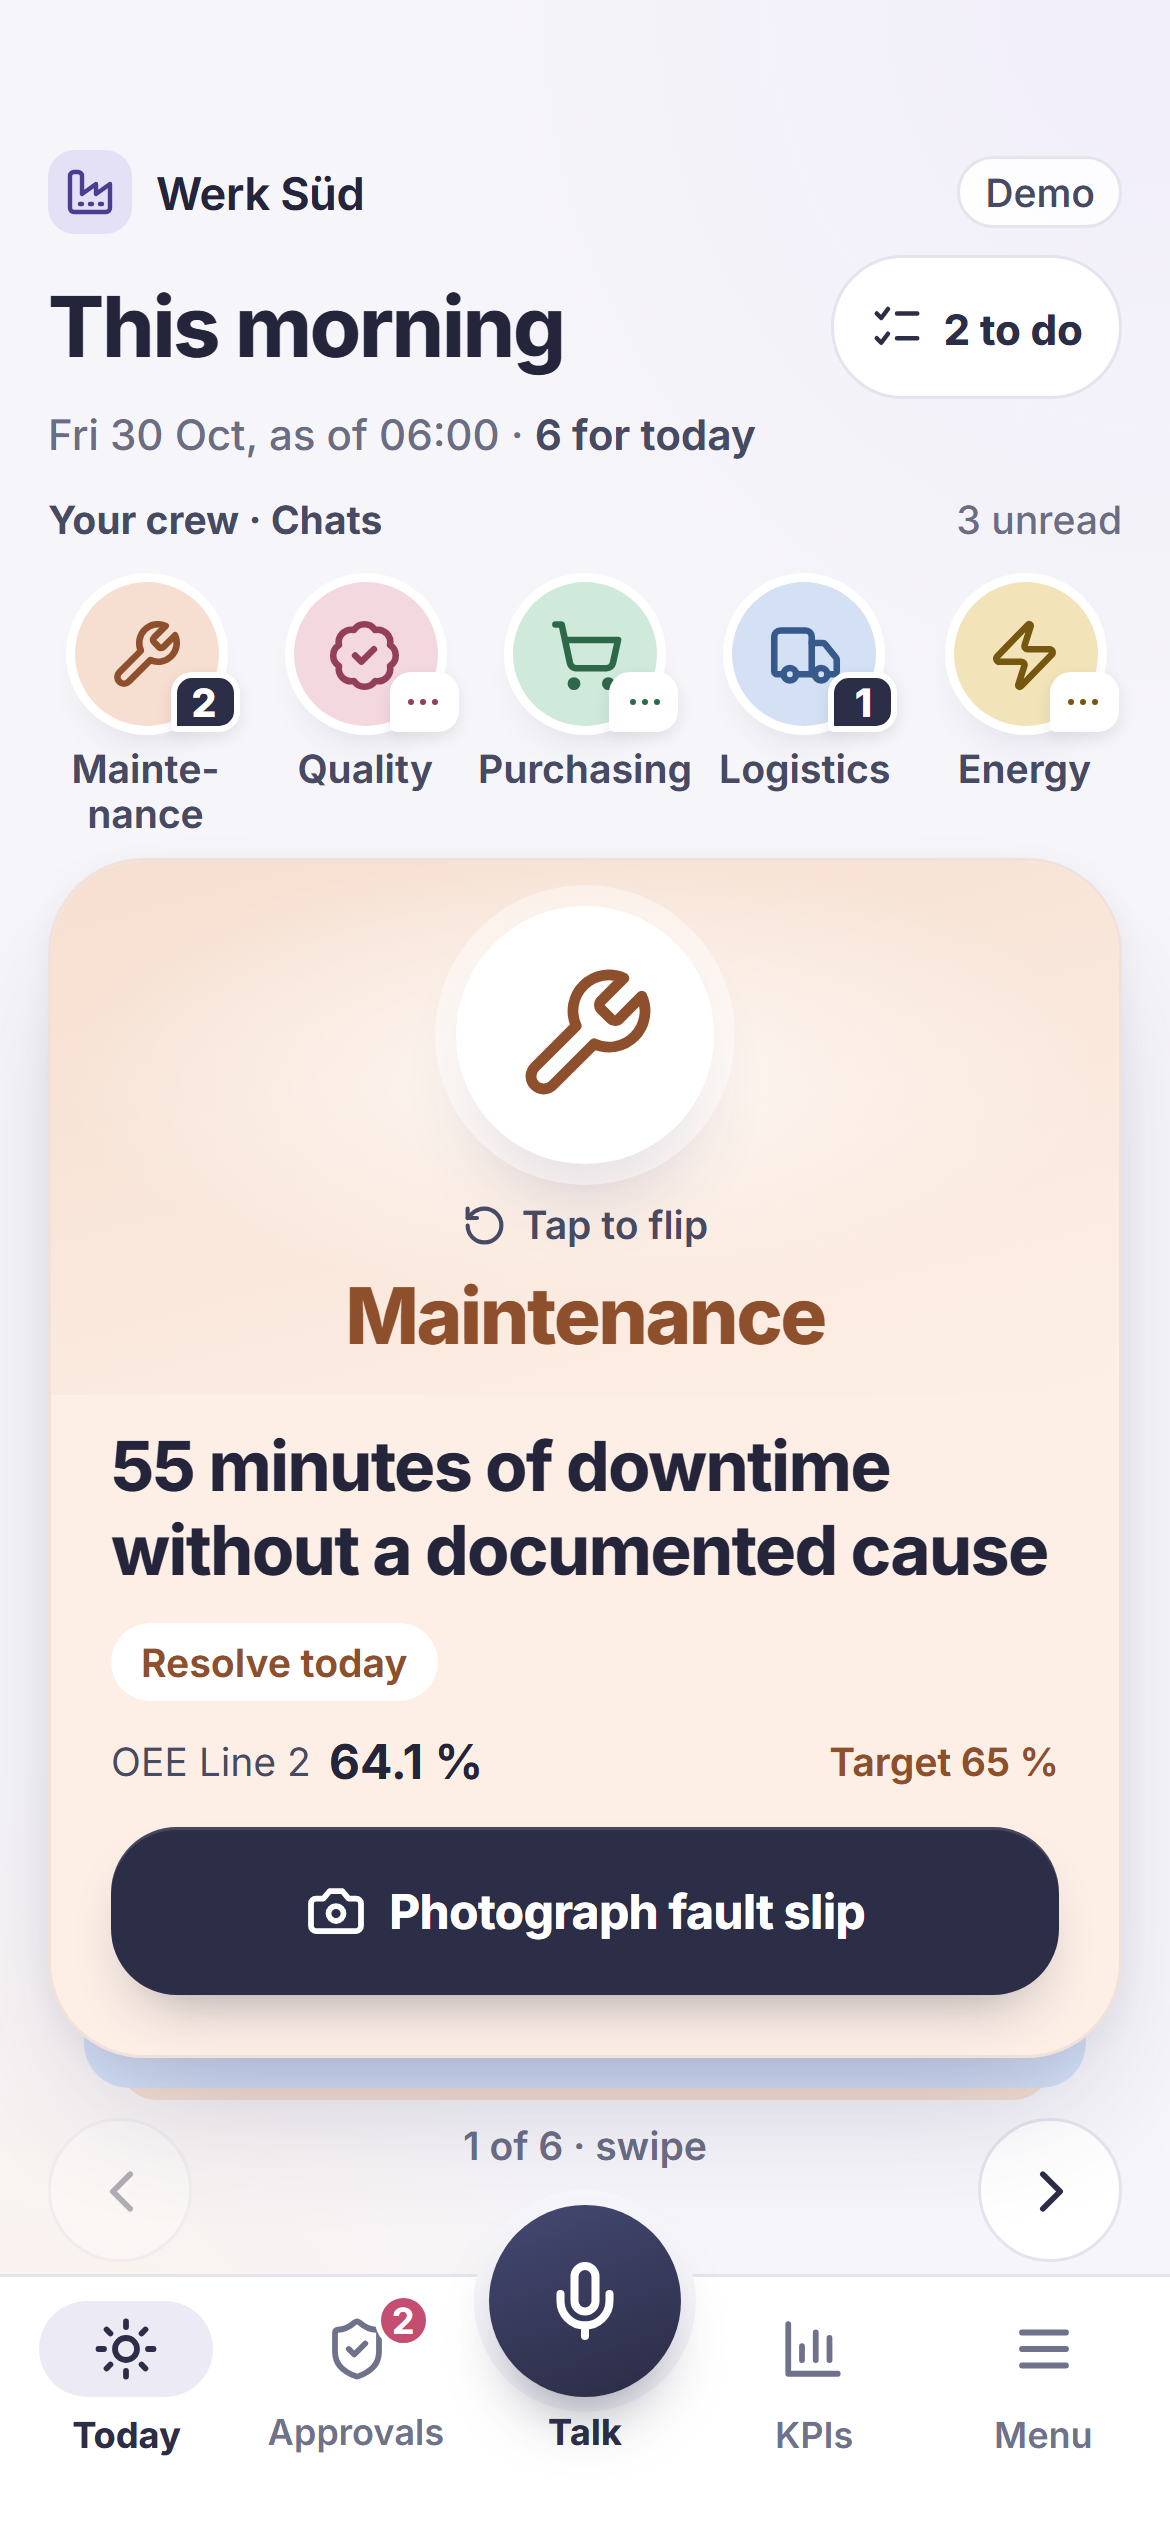
Daily overview with the crew and anomalies in Werk Süd

Find where your plant has potential.

An initial analysis of your existing operational data shows which anomalies deserve closer investigation. Every finding includes the underlying data. The initial analysis is free of charge.

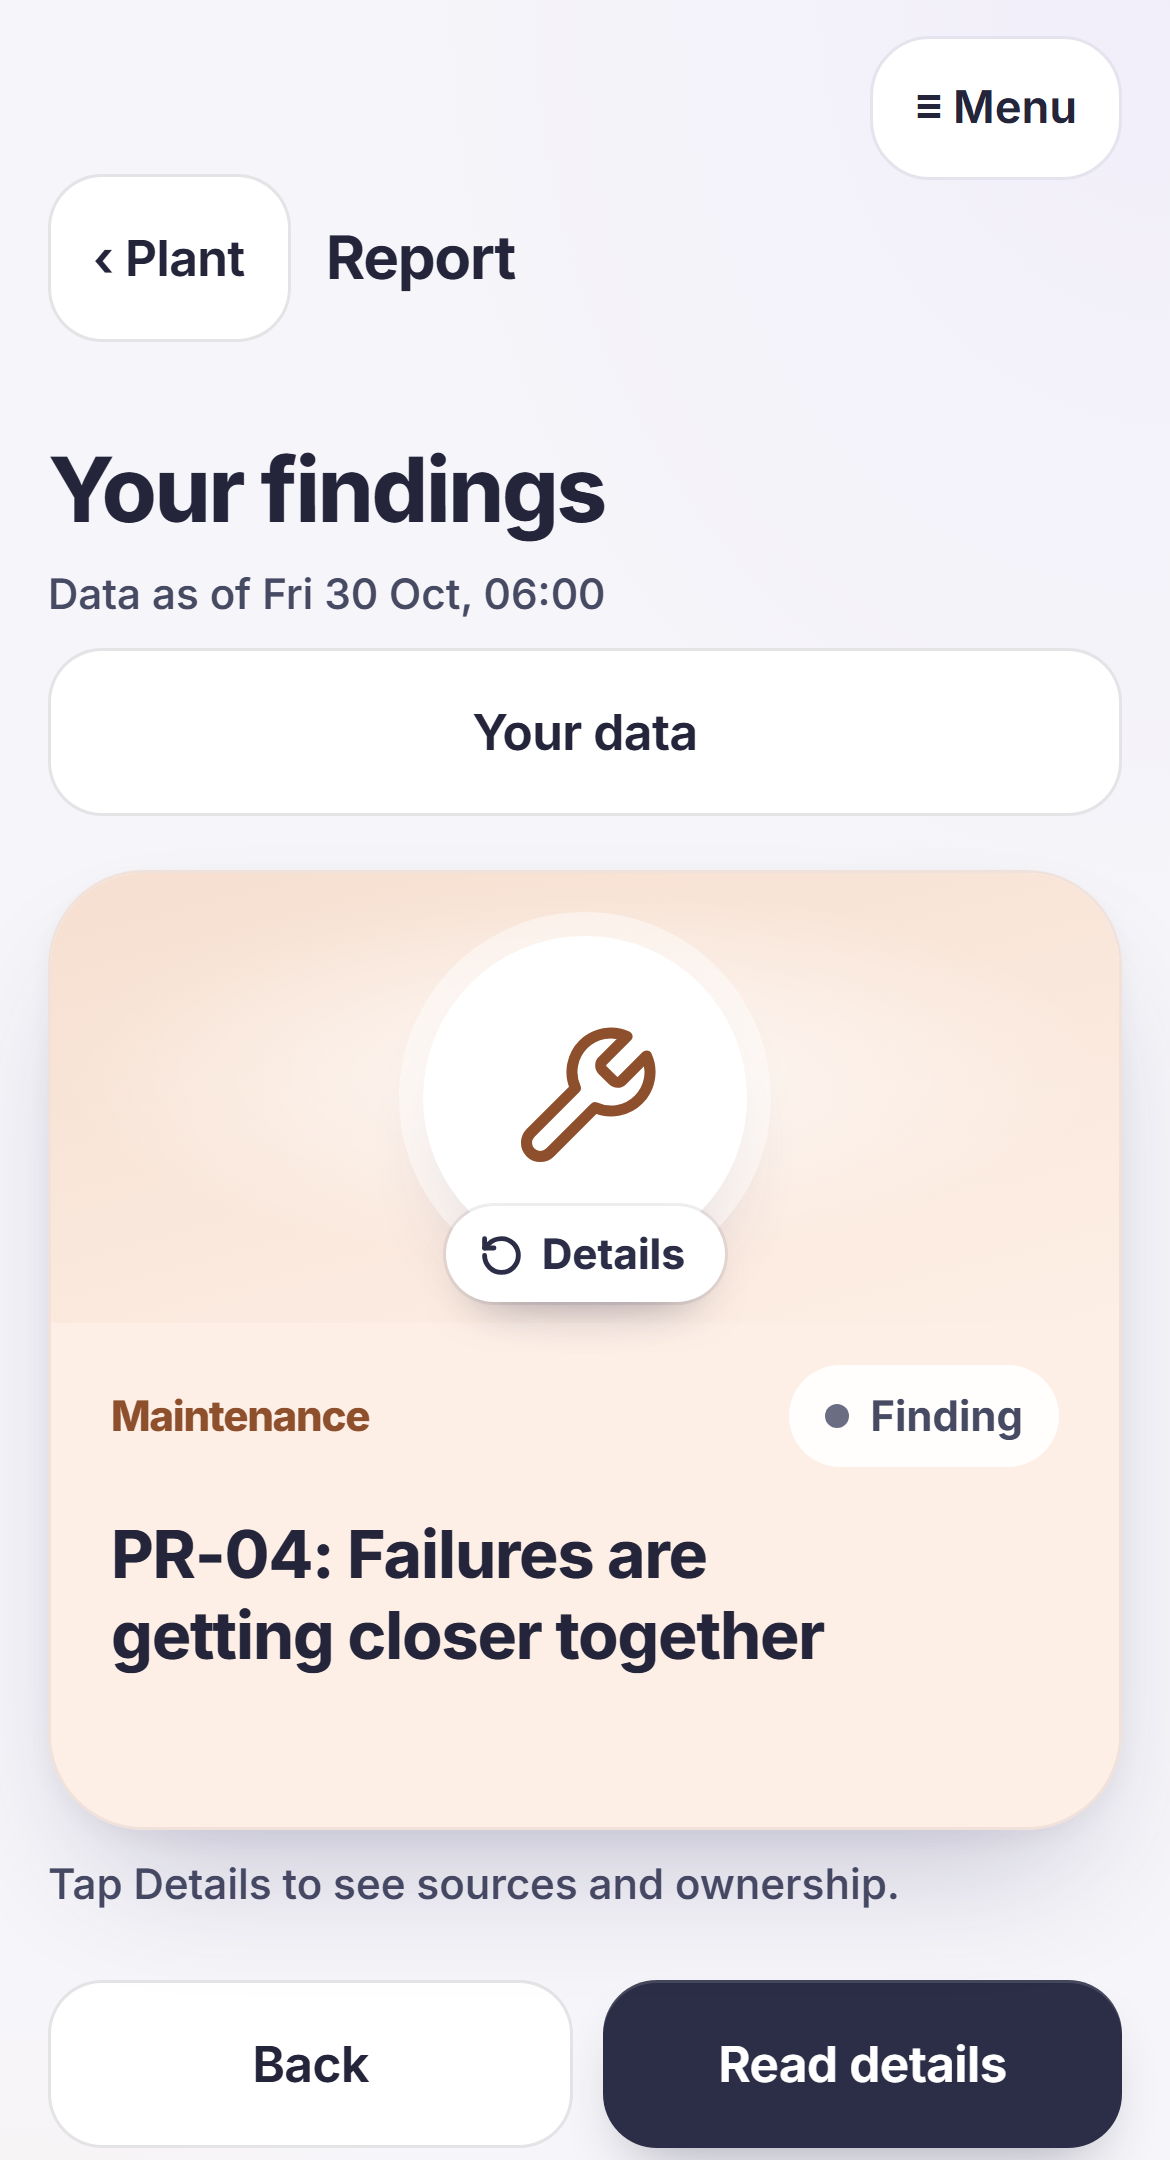
Source-backed findings in Werk Süd
Werk Süd · Findings from export data

90 days to assess the value in your plant.

  1. Before

    Initial analysis, free of charge. We choose the area together.

  2. Days 30 and 60

    Interim review with your team.

  3. Day 90

    Joint review with your controlling team.

The pilot starts after technical setup and joint confirmation of the baseline values.

From findings to action.

Your data guides action: manage loads, adjust settings and plan maintenance. With approval, a receipt and undo.

Limit loads. Switch to standby.

The crew limits loads and switches approved equipment to standby.

Werk Süd

View execution and measurement
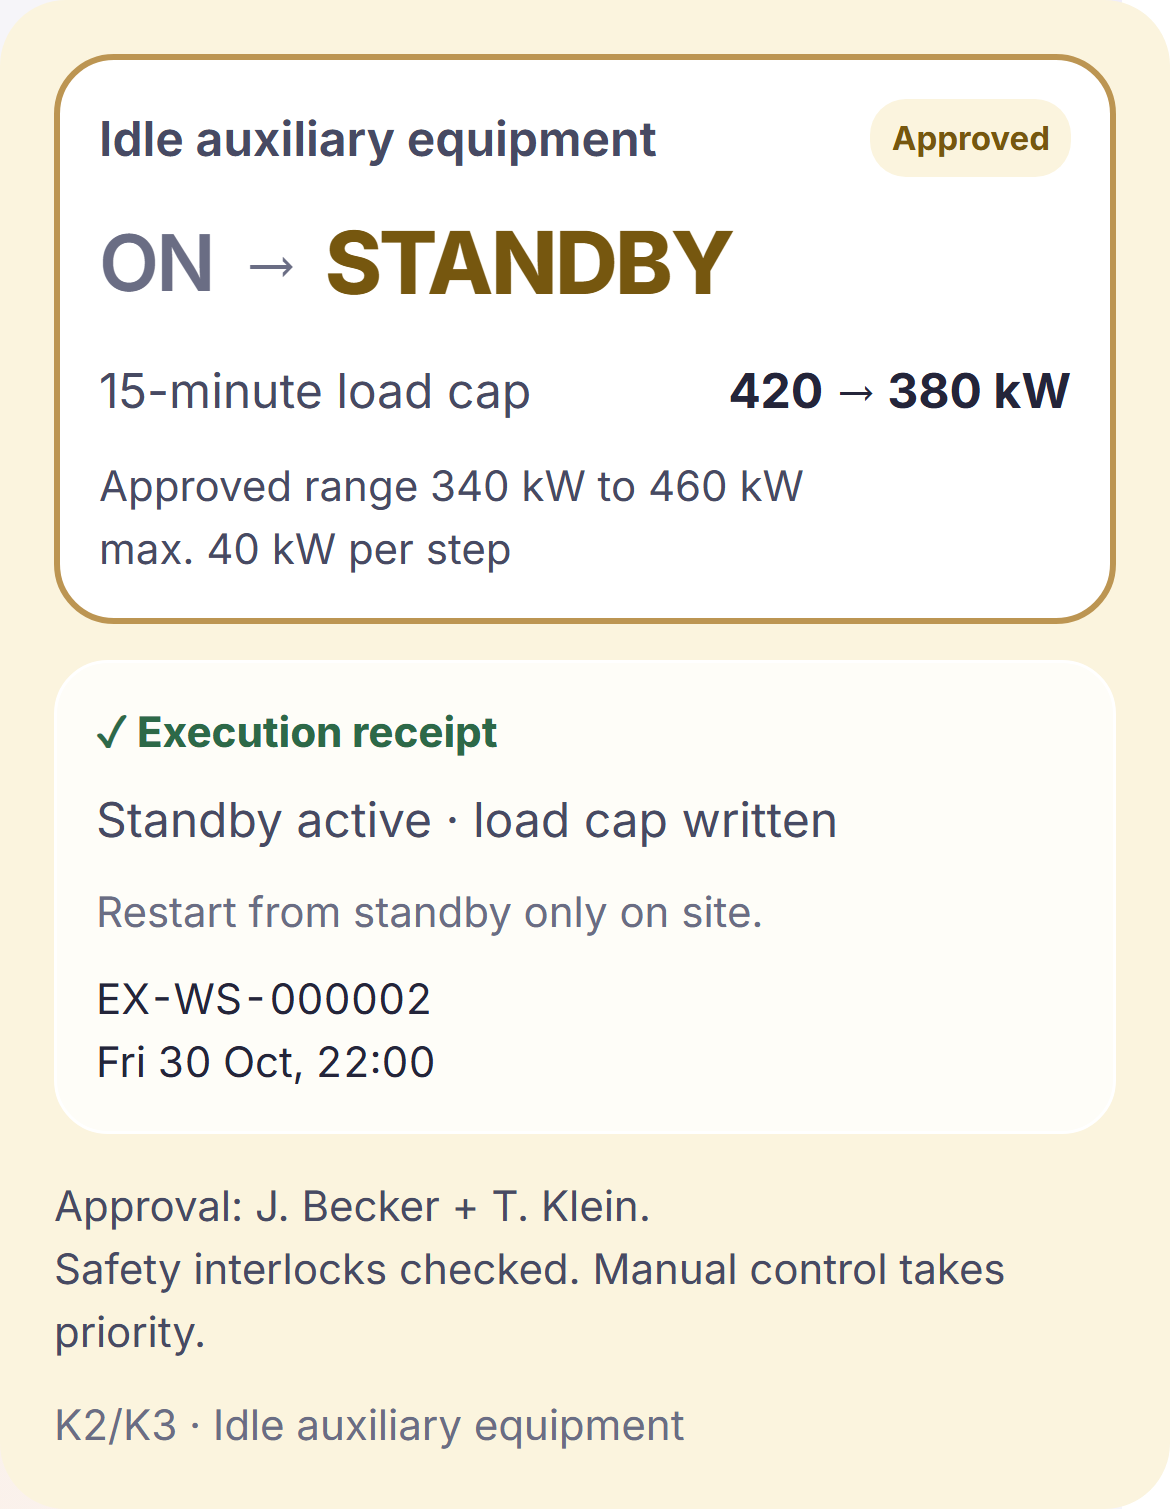
Energy: idle auxiliary equipment on standby, load cap 420 to 380 kW, two approvals.
Idle auxiliary equipment switches to standby. The 15-minute load cap falls from 420 to 380 kW.
  • K2 · Operating modeON → STANDBY
  • K3 · Operating modeON → STANDBY
  • WERK-LAST · 15-minute load cap420 kW → 380 kW
Technical details and receipt

WERK-LAST · Approved range: 340 kW to 460 kW; maximum per step: 40 kW

Executed

Receipt
EX-WS-000002
Time
Approval
J. Becker, T. Klein
Rule
Two separate approvalsRange and safety interlocks checked

Follow-up values

Follow-up values are reported separately from historical export data. They do not establish a causal effect.

Energy in the comparison window: 120 → 95 kWh · Follow-up hour

Peak load: 420 → 380 kW · Follow-up hour

If follow-up values get worse, the stored rule resets the setting automatically. A manual rollback by the approving person or plant leadership requires a reason, satisfied safety interlocks and no critical operation, newer setting or manual takeover. Restart from standby requires someone on site.
Adjust within approved bands.

The crew adjusts settings within approved bands, measures quality and resets the setting if needed.

Werk Süd

View execution and measurement
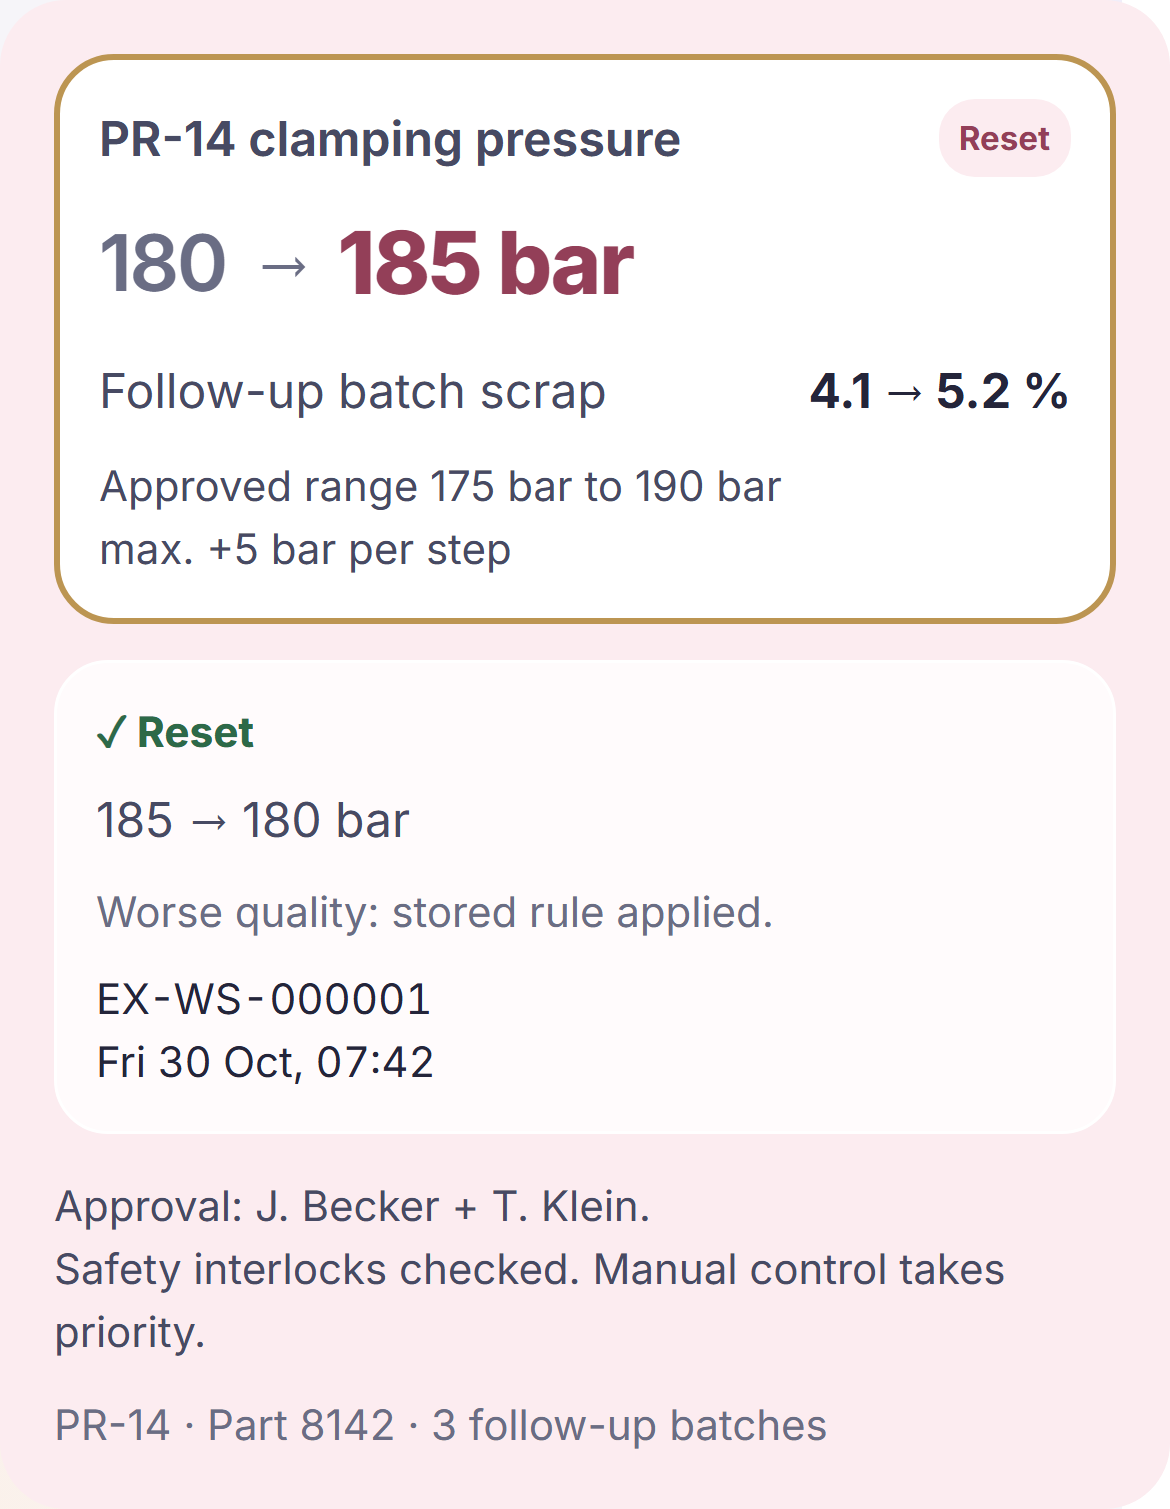
PR-14: clamping pressure 180 to 185 bar, worse quality and reset to 180 bar.
In this example, quality gets worse. The setting is reset according to the stored rule.
  • PR-14 · Clamping pressure180 bar → 185 barReset to: 180 bar
Technical details and receipt

PR-14 · Approved range: 175 bar to 190 bar; maximum per step: +5 bar

Reset

Receipt
EX-WS-000001
Time
Approval
J. Becker, T. Klein
Rule
Two separate approvalsRange and safety interlocks checked

Follow-up values

Follow-up values are reported separately from historical export data. They do not establish a causal effect.

Scrap in follow-up batches: 4.1 → 5.2 % · 3 follow-up batches of part 8142

Reset at Fri 30 Oct, 08:00: Follow-up batches worse than the comparison baseline. Automatically by the stored rule.

If follow-up values get worse, the stored rule resets the setting automatically. A manual rollback by the approving person or plant leadership requires a reason, satisfied safety interlocks and no critical operation, newer setting or manual takeover.

Reduce speed. Plan stop windows.

The crew reduces speed and plans maintenance with a notification and order.

Werk Süd

View execution and measurement
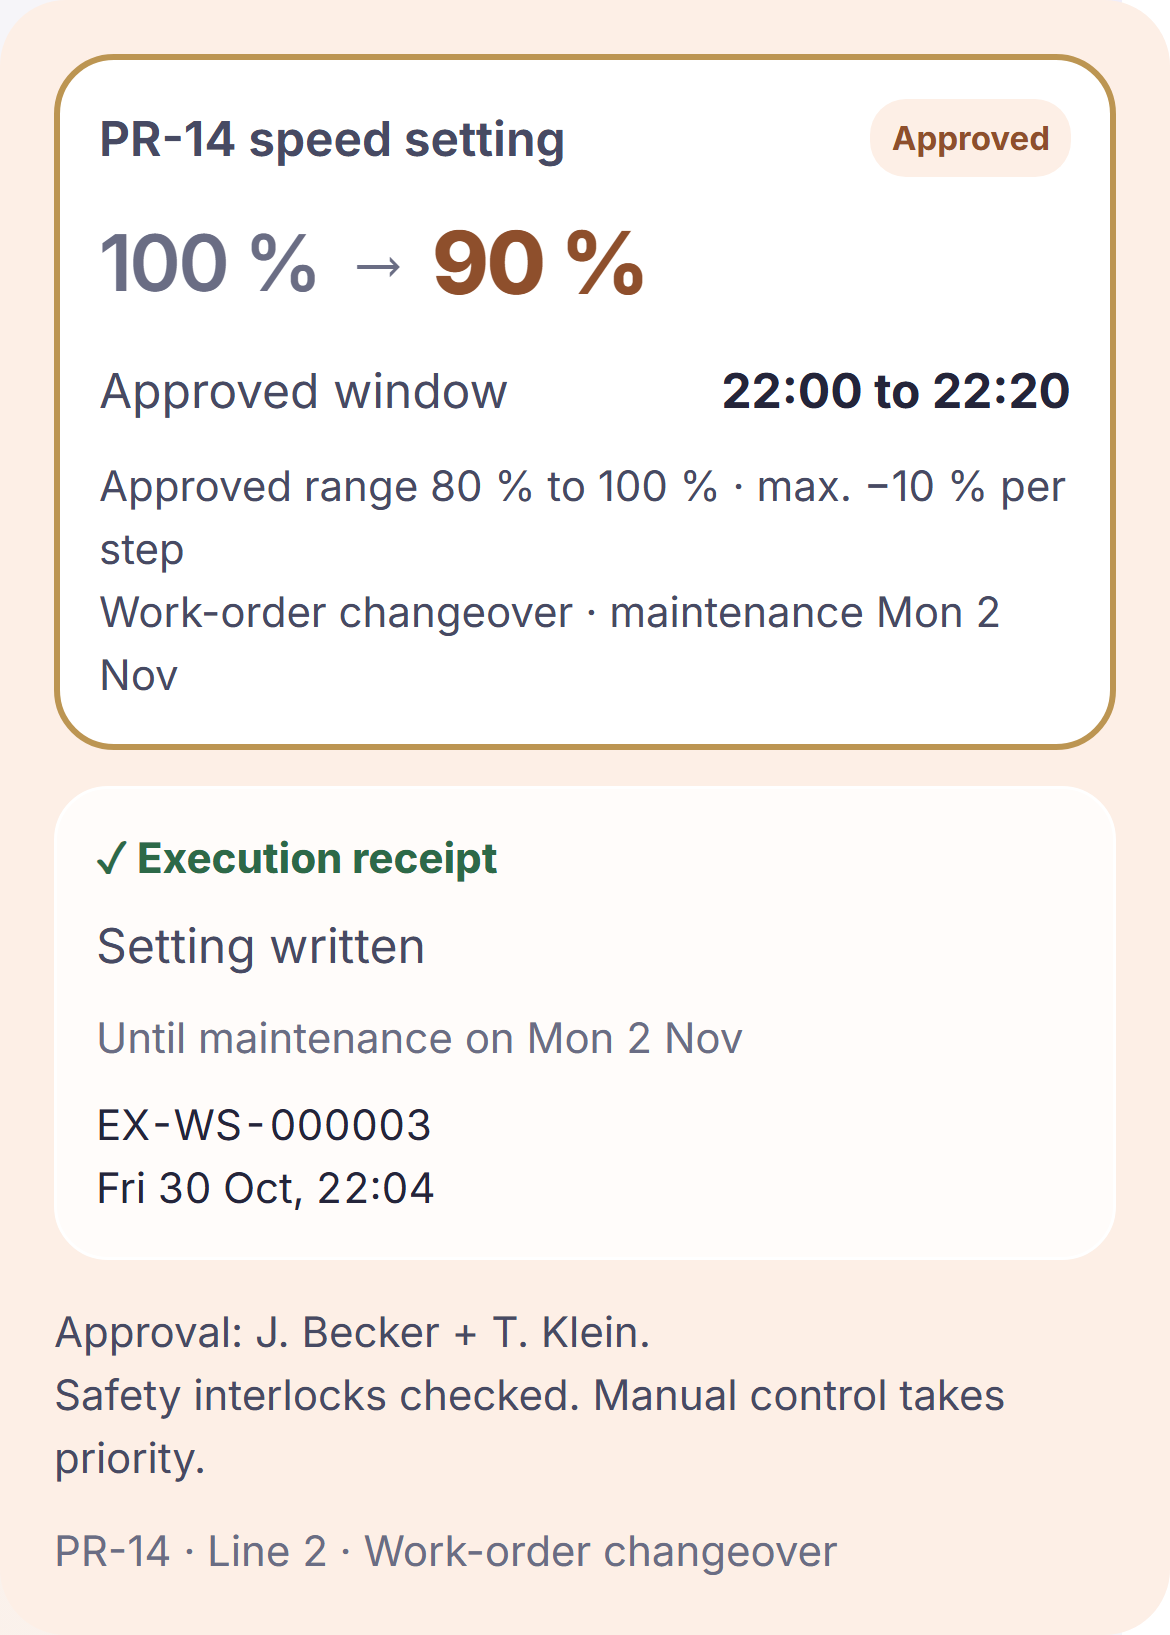
PR-14: speed 100 to 90 %, window 22:00 to 22:20, maintenance Mon 2 Nov.
Speed is reduced to 90 % during the approved work-order changeover from 22:00 to 22:20. Maintenance is planned for Mon 2 Nov.
  • PR-14 · Speed100 % → 90 %
Technical details and receipt

PR-14 · Approved range: 80 % to 100 %; maximum per step: −10 %

Approved window: 22:00 to 22:20 during the work-order changeover. Maintenance: Mon 2 Nov.

Executed

Document
IM-WS-000001, IA-WS-000002
Receipt
EX-WS-000003
Time
Approval
J. Becker, T. Klein
Rule
Authorized approvalTwo separate approvalsRange and safety interlocks checked

Follow-up values

Follow-up values are reported separately from historical export data. They do not establish a causal effect.

Unplanned stoppage minutes: 55 → 20 min · 3 follow-up work orders after the order change

If follow-up values get worse, the stored rule resets the setting automatically. A manual rollback by the approving person or plant leadership requires a reason, satisfied safety interlocks and no critical operation, newer setting or manual takeover.

You set the limits.

You set equipment, parameters and roles. The crew checks before every action.

  • Approved bands

    Value ranges, maximum steps and minimum intervals bound every change.

  • Safety interlocks

    Safety interlocks prevent unsafe changes. Missing interlocks and critical operations block machine changes.

  • Two-person approval

    Every machine action needs approval from two responsible people.

  • Manual override

    The operator takes over on site. Further writes stay blocked.

  • Undo

    If follow-up values get worse, the stored rule resets the setting automatically. The approving person or plant leadership can roll back by hand only when safety interlocks are met and there is no newer setting or manual takeover. No automatic restart from standby.

  • Full action log

    The rule, approval, before-and-after values, measurements and reversal stay traceable.

SAP, MES and control systems remain the systems of record. We agree on data scope and access rights before the pilot.

Measured on your KPIs.

You choose the KPIs. The app documents their development and the related actions. We assess the economic value together with your controlling team.

Metrics in Werk Süd with access to source data
Werk Süd · Metrics and sources

Where could getAdvantage support your plant?

Let’s discuss which area would be suitable for a pilot. In the first conversation, we review your starting point and available data.

Marc LindnerCo-Founder & Chief Growth Officermarc@getadvantage.app

* Required fields

Benjamin Hellmich
Benjamin HellmichCo-Founder & CEO
Marc Lindner
Marc LindnerCo-Founder & Chief Growth Officer

Register release interest

Get the release update on how your crew works on your machines and in your systems. Leave your contact details and we’ll keep you informed.

* Required fields

No commitment. Registered only after email confirmation. Withdraw at any time.